Welcome to Vbond
Wind Load + Poor Folding = Disaster: Understanding Alucobond Edge Stress
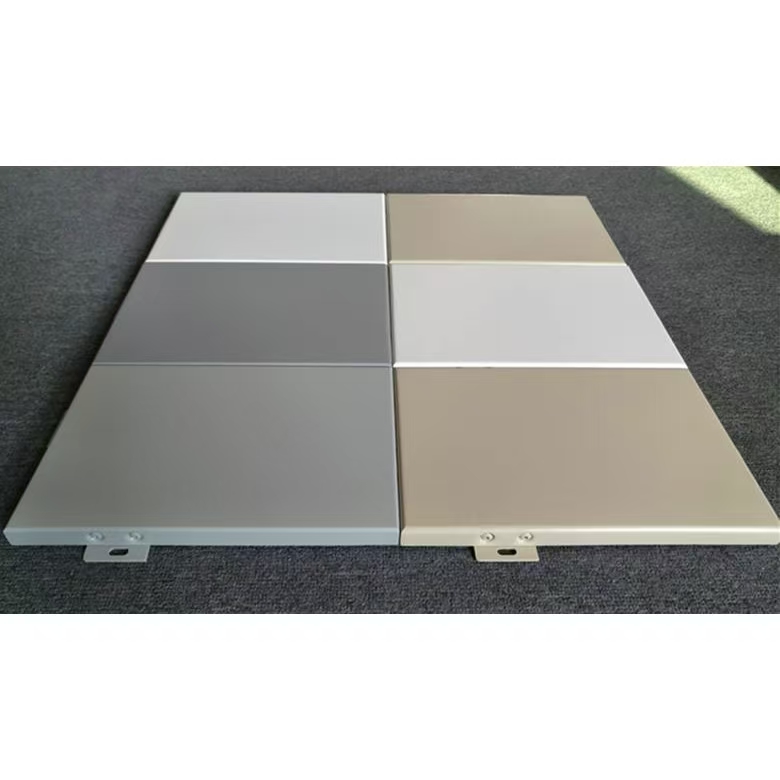
Wind Load + Poor Folding = Disaster: Understanding Alucobond Edge Stress
You spec the right panel. You check the wind load calculations. The facade goes up looking perfect.
Then the first storm hits. Or maybe the second. Or the third.
Suddenly, you see cracks along the folded edges. Not big ones at first. Just hairline fractures. But they grow. They spread. And now you have a problem.
What went wrong?
The panels didn't fail because the wind was too strong. They failed because poor folding created stress points. The wind just finished the job.
This guide explains the connection. You will learn how wind loads stress panel edges. You will understand why some folds fail and others don't. And you will know exactly what to specify to prevent failure.
How Wind Actually Loads a Facade Panel
Wind does not push evenly on a building.
It pushes harder on some areas than others. Corner zones experience suction forces two to three times higher than the center of the wall. Parapet edges take the worst of it.
Wind exerts two distinct forces:
- Positive pressure pushes the panel inward.
- Negative pressure (suction) pulls the panel outward.
Negative pressure often governs the design. It can be significantly higher than positive pressure on the same surface.
For a typical high-rise facade, design wind loads reach 2.0 to 5.0 kPa. That is substantial force on a 4mm panel.
Now add the fatigue factor. Wind is not a one-time event. It cycles. Every gust loads the panel. Every gust unloads it. Over years, that cyclic loading adds up.
Research shows the fatigue limit of aluminum composite panel material is around 2.3 MPa. Exceed that repeatedly, and you get progressive damage.
The Fold: Your Panel's Weakest Link
Here is the thing about folded edges. They are not as strong as the flat panel.
The folding process work-hardens the aluminum. That makes it harder. It also makes it more brittle. Less ductile metal cannot absorb as much stress before cracking.
The V-groove makes it worse.
To fold a panel, you route a groove into the back side. That groove removes the core and part of the rear aluminum skin. What remains is called residual thickness.
Standard residual thickness for a 4mm panel is 0.3 to 0.5mm. That thin layer of aluminum carries all the stress at the fold.
Now think about what happens under wind load. The panel flexes. That flexing concentrates at the fold line. The thin residual aluminum takes the brunt of it.
If the residual thickness is too thin, the fold cracks. If the bend radius is too tight, the stress concentration increases. If the groove is inconsistent, you get weak spots.
How Poor Folding Creates a Disaster Waiting to Happen
Let us walk through the failure sequence.
Step one: Bad folding.
The fabricator uses a tight bend radius. They want sharp corners. The panel looks great coming off the brake.
But the tight radius stretches the outer aluminum skin beyond its limit. Micro-cracks form at the fold. You cannot see them. They are too small.
Step two: Thermal cycling.
The sun heats the panel. The core expands faster than the skins. The fold flexes. The micro-cracks grow a little.
Night comes. The panel cools. The cracks grow a little more.
Repeat this every day for two years.
Step three: Wind load.
A storm hits. The wind pressure bends the panel. That bending concentrates right at the fold line.
The micro-cracks are now big enough to see. Hairline fractures appear along the edge.
The panel has failed.
The Numbers: What the Research Shows
Studies on aluminum composite panel fatigue under wind loading reveal some hard numbers:
- Fatigue limit of ACP material: approximately 2.3 MPa
- Safe wind speed for a 0.8 m² panel: 14.8 m/s
- A 4mm hole (for fasteners) reduces safe wind speed by about 25%
Wind load testing standards like ASTM E330 and EN 12179 certify panel resistance at specified pressures. But these tests measure static load capacity. They do not always capture cumulative fatigue from years of cycling.
That is why folded edge quality matters so much. A panel that passes a static wind test can still fail from fatigue if the fold has micro-cracks.
The Critical Parameters That Determine Fold Strength
Parameter | What It Should Be | Why It Matters |
Minimum bend radius | 60mm for 3mm panel; 80mm for 4mm panel | Tighter radius = more stress concentration |
Residual thickness | 0.3 to 0.5mm for 4mm panel | Too thin = cracks; too thick = excess stress |
Groove consistency | Within ±0.1mm across all panels | Variation creates weak spots |
Bending temperature | Above 50°F (10°C) | Cold aluminum is brittle |
Single bending only | No re-bending | Re-bending creates micro-cracks |
Caption: Critical folding parameters for wind-resistant Alucobond edges. Source: Industry fabrication standards.
Alt text: Table showing minimum bend radius, residual thickness, groove consistency, bending temperature, and single bending requirements for aluminum composite panel folds.
Why Some Panels Fail and Others Don't
The difference is not luck. It is discipline.
Panels that survive wind loads have:
- Correct temper (H22 or H42) – not too hard, not too soft
- Residual thickness of 0.3mm or more – enough material to absorb stress
- Bend radius that meets minimums – 60mm for 3mm, 80mm for 4mm
- Warm bending conditions – above 65°F
- Precise, consistent routing depth – no variation
- Single bending – no do-overs
Panels that fail have the opposite.
What to Specify in Your Procurement Documents
Procurement professionals, here is your checklist.
1. Bend radius requirement.
Write this clearly: "Minimum inside bend radius of 80mm for 4mm panels. No exceptions."
Do not accept "we can make it tighter and it will look better." Sharp corners look nice. They also crack.
2. Residual thickness verification.
Require micrometer measurements. Every batch. Ask for the records.
If the supplier cannot show you residual thickness data, find another supplier.
3. No re-bending policy.
Specify: "Any panel that requires re-bending shall be scrapped and replaced at fabricator's expense."
Re-bending creates micro-cracks. Micro-cracks grow under wind load.
4. Temperature requirements.
Require bending at ambient temperature above 65°F (18°C).
Cold panels crack. It is that simple.
5. Tested fastening systems.
Specify engineered fixing systems that allow for thermal movement.
Over-tightened fasteners restrict movement. Restricted movement forces stress into the fold.
Wind Load Considerations for Your Specification
Do not guess at wind loads. Use the numbers.
- Design wind load for typical facades: 2.0 to 5.0 kPa
- Corner and parapet zones: 2–3 times higher than wall center
- Minimum design wind load: 20 psf (about 1.0 kPa), with 40 psf on parapet and corner panels
Specify panels tested to ASTM E330 or EN 12179. But remember: static testing is not fatigue testing. A panel that passes static load can still fail from years of wind cycling.
That is why fold quality is non-negotiable.
What to Do If You See Cracks
Cracks along folded edges do not heal. They grow.
Do not patch them with filler. Filler does not restore structural integrity. The panel will fail under the next wind load.
Do not ignore them. Small cracks become big cracks. Big cracks compromise the entire panel.
Replace the affected panels. Match the batch number for color consistency.
The Bottom Line
Wind load and poor folding are a deadly combination.
The wind provides the force. The poor fold provides the weak point. Together, they create failures that could have been prevented.
You cannot control the wind. You can control the fold.
Specify the right bend radius. Verify residual thickness. Require single bending. Insist on proper temperature. Use engineered fastening systems.
Do these things, and your panels will stand up to wind loads for decades.
Ignore them, and you will be answering phone calls after the next storm.
The choice is yours.