Welcome to Vbond
How to Avoid Core Thickness Variations in Your Aluminum Composite Panel Order
How to Avoid Core Thickness Variations in Your Aluminum Composite Panel Order
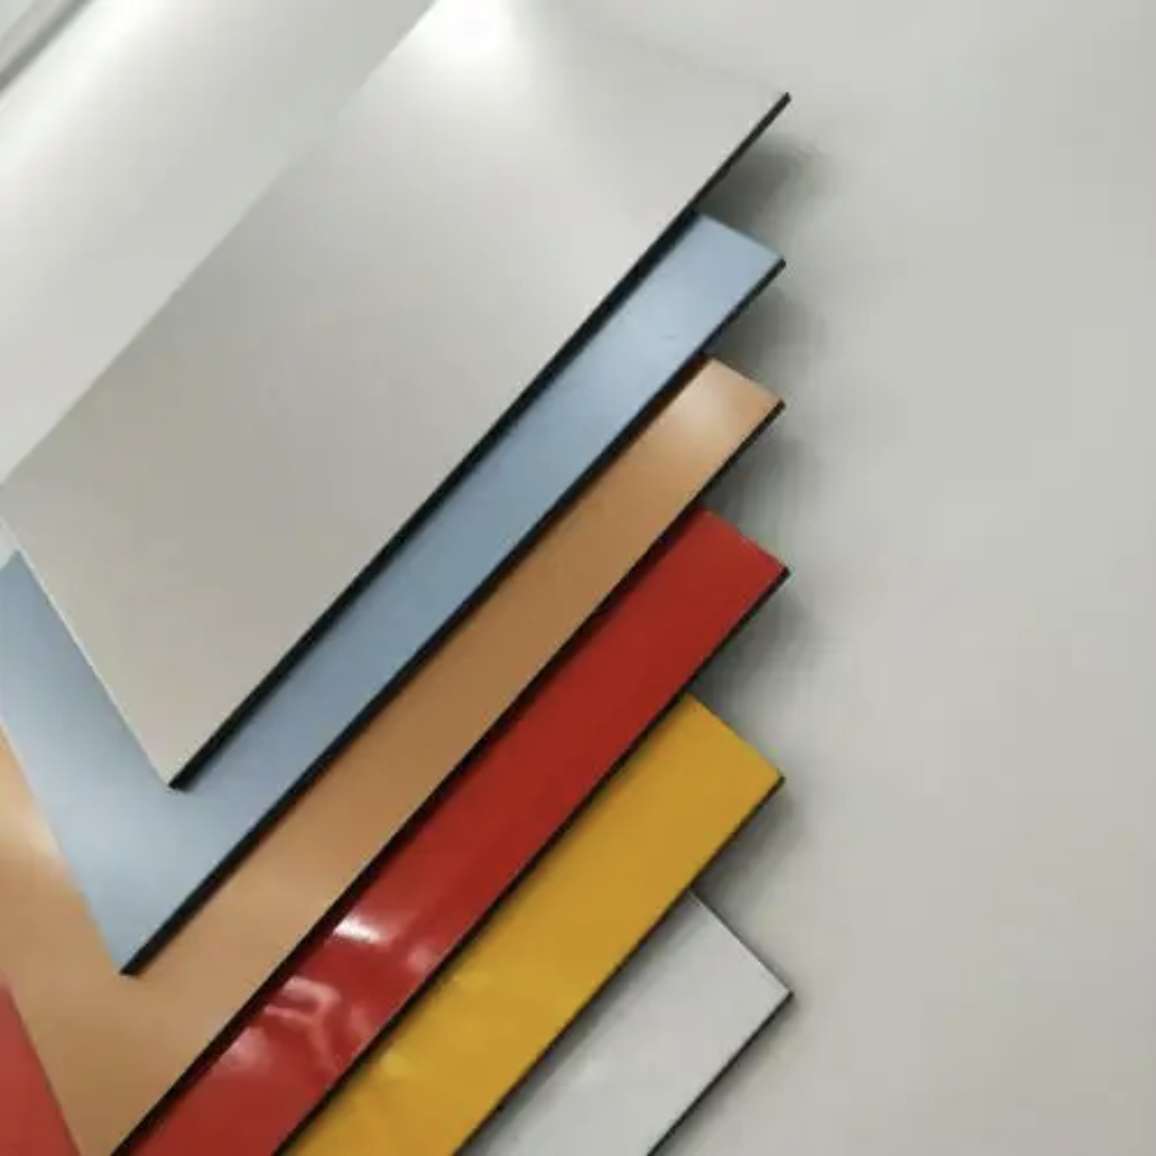
For procurement professionals and facade contractors, consistency is everything. When you specify an aluminum composite panel (ACP) with a particular thickness—whether 3mm, 4mm, or 6mm—you expect every panel in the shipment to meet that dimension within a narrow tolerance. Unfortunately, core thickness variation is a common and often overlooked quality issue that can cause significant problems during installation and compromise the long-term performance of the facade.
Core thickness variation refers to the inconsistent thickness of the middle layer (the core) between the two aluminum skins. This variation can occur within a single panel, between panels in the same batch, or across different batches in the same shipment.
This guide explains why core thickness variation occurs, how it affects your project, what tolerances are acceptable, and how procurement professionals can ensure that their aluminum composite panel order arrives with consistent, specification-compliant core thickness.
What Is Core Thickness Variation?
An aluminum composite panel consists of three layers:
- Top aluminum skin (typically 0.15mm to 0.50mm)
- Core material (polyethylene, fire-retardant mineral, or A2 non-combustible mineral)
- Bottom aluminum skin (typically 0.15mm to 0.50mm)
The total panel thickness is the sum of these three layers. However, when we refer to "core thickness variation," we mean inconsistencies in the core layer itself—not simply the total panel thickness.
For example, a specified 4mm panel with 0.50mm skins should have a core thickness of approximately 3.00mm (4.00mm total minus 0.50mm top skin minus 0.50mm bottom skin). Core thickness variation occurs when the core measures 2.80mm in some areas and 3.20mm in others.
Why Core Thickness Variation Matters
Core thickness is not merely a dimensional specification. It directly affects:
Impact Area | Consequence of Core Thickness Variation |
Panel flatness | Uneven core thickness causes bowing, warping, or oil canning after installation. |
Structural integrity | Thinner core areas have reduced mechanical strength and impact resistance. |
Fire performance | For FR and A2 cores, thickness variation means inconsistent fire protection across the panel. |
Fabrication | Varying thickness makes bending, folding, and routing unpredictable; tools must be constantly adjusted. |
Installation | Panels of inconsistent thickness do not align properly, resulting in uneven joints and reveals. |
Aesthetics | Visible distortion and waviness ruin the visual quality of the finished facade. |
Root Causes of Core Thickness Variation
To prevent core thickness variation, procurement professionals must understand why it happens.
1. Inconsistent Laminating Pressure
During manufacturing, the aluminum skins and core material are bonded together under heat and pressure using large laminating rollers. If the pressure applied across the width of the rollers is not perfectly uniform, the core will be compressed more in some areas than others.
Result: Thinner core at the edges or center of the panel, depending on roller pressure distribution.
2. Variation in Core Material Extrusion
Core materials (especially polyethylene and mineral-filled composites) are produced by extrusion. If the extrusion process has fluctuations in temperature, screw speed, or die opening, the resulting core sheet will have thickness variations before it even enters the laminator.
Result: Incoming core material that is already out of tolerance.
3. Roller Wear and Misalignment
Laminating rollers wear over time. Worn rollers develop uneven surfaces that transfer imperfections to the panel. Misaligned rollers apply pressure at an angle, creating a wedge-shaped panel that is thicker on one edge than the other.
Result: Progressive core thinning at the center (worn rollers) or tapered thickness from edge to edge (misalignment).
4. Cooling Rate Inconsistency
After lamination, the panel passes through cooling rollers or a cooling bath. If cooling is uneven, the core material may contract unevenly across the panel, creating residual stresses and thickness variations after the panel has cooled completely.
Result: Panels that measure correctly at the factory but warp or change thickness after shipment.
5. Core Material Batch Variation
Different batches of core material may have different flow characteristics, density, or compressibility. If a manufacturer switches batches mid-order without adjusting laminating parameters, thickness variation will occur between panels produced before and after the switch.
Result: Inconsistent thickness across different bundles within the same shipment.
Acceptable Core Thickness Tolerances
Industry standards specify acceptable tolerances for total panel thickness. From these, we can infer an acceptable core thickness variation.
Standard | Specified Panel Thickness | Acceptable Tolerance (Total Panel) |
ASTM D7791 | 3 mm | ±0.10 mm |
ASTM D7791 | 4 mm | ±0.12 mm |
ASTM D7791 | 6 mm | ±0.15 mm |
EN 13523 (typical) | 3–6 mm | ±0.10–0.15 mm |
What this means for core thickness: If total panel tolerance is ±0.12mm for a 4mm panel, and aluminum skin thickness is consistent (±0.02mm), then core thickness variation should not exceed approximately ±0.08–0.10mm across the panel and across the shipment.
Practical guidance: Reject panels where core thickness variation exceeds 0.15mm within a single panel, or where average core thickness differs by more than 0.10mm between panels in the same shipment.
How to Inspect for Core Thickness Variation
Procurement professionals and site supervisors can perform the following inspections upon delivery:
1. Total Panel Thickness Measurement
Tool: Digital caliper (calibrated, resolution 0.01mm)
Procedure:
- Measure at least 10 locations per panel (four corners, four edges, center).
- Measure at least 10% of panels per bundle, selected randomly.
- Record maximum, minimum, and average thickness.
Red flags:
- Any measurement outside specified tolerance (±0.10–0.15mm depending on thickness)
- Variation greater than 0.10mm between the thickest and thinnest measurements on a single panel
- Significant difference between the average thickness of different bundles
2. Edge Inspection
Tool: Magnifying glass or loupe (10x–20x)
Procedure:
- Examine the cut edge of the panel.
- Look for visible waviness or unevenness in the core layer.
- Check if the core appears consistently centered between the two aluminum skins.
Red flags:
- Core visibly thicker on one edge than the other (tapered panel)
- Wavy or irregular core profile along the cut edge
- Core not centered (thicker near top skin, thinner near bottom skin)
3. Flatness Test
Tool: Straightedge (2 meters long) and feeler gauge
Procedure:
- Place the straightedge across the panel width (short dimension) and length (long dimension).
- Insert feeler gauge at the point of maximum gap between panel and straightedge.
- Measure bow, warp, or twist.
Red flags:
- Bow exceeding 0.5% of panel length (e.g., 2mm over 4m length)
- Any visible twist or saddle shape
- Panels that do not lie flat on a level surface
4. Destructive Sampling (For Critical Projects)
Procedure:
- Cut a panel cross-section (at least 50mm wide across the full panel width).
- Measure core thickness at multiple points across the cut section using calipers or a microscope.
- Compare measurements to specifications.
Note: This test destroys the panel. Perform on a representative sample, not on the entire shipment.
Procurement Strategies to Prevent Core Thickness Variation
The most effective way to avoid core thickness variation is to prevent it before the panels are manufactured and shipped. Implement these strategies:
1. Specify Tolerances in Your Purchase Order
Do not simply specify "4mm panel." Write:
"Total panel thickness: 4.0 mm ±0.10 mm. Core thickness variation across any single panel shall not exceed 0.10 mm. Core thickness variation between panels within the same shipment shall not exceed 0.10 mm average difference."
2. Require Manufacturing Process Documentation
Ask potential suppliers to provide:
- Laminating roller calibration records (showing uniform pressure distribution)
- Core material incoming inspection reports (verifying thickness consistency before lamination)
- In-process thickness monitoring data (continuous or high-frequency sampling)
3. Request Pre-Production Samples
Before full manufacturing begins, request:
- A pre-production sample of at least 5–10 panels from the actual production line that will be used for your order.
- Thickness measurement data for each sample panel (minimum 10 locations per panel).
- A cut cross-section of one sample panel showing core uniformity.
4. Conduct Third-Party In-Process Inspection
Engage an independent inspector to be present at the factory during manufacturing. The inspector should:
- Verify laminating roller pressure settings and calibration.
- Randomly measure panel thickness during production (not just at final inspection).
- Flag any drift in thickness measurements immediately.
5. Include a Rejection Clause
Specify in your contract:
"If more than 5% of panels in any shipment exceed the specified thickness tolerance, or if any panel shows core thickness variation greater than 0.15mm, the Buyer reserves the right to reject the entire shipment at the Supplier’s expense, including return freight and replacement costs."
Supplier Selection Criteria
When evaluating aluminum composite panel suppliers, prioritize those who demonstrate:
Criteria | What to Look For |
ISO 9001 certification | Documented quality management system, including process control for thickness consistency. |
Modern laminating line | Hydraulic or servo-controlled rollers with continuous thickness monitoring. |
Incoming core inspection | Quality checks on core material thickness before lamination. |
Statistical process control (SPC) | Real-time data collection and analysis of thickness measurements during production. |
Third-party thickness verification | Willingness to allow independent inspection of thickness during and after production. |
Red Flags in Supplier Responses
Be cautious if a supplier:
- Cannot specify their thickness tolerance in writing.
- Refuses to provide pre-production samples.
- Has no documented process for measuring core thickness consistency.
- Offers significantly lower prices than competitors (pressure to cut costs often leads to relaxed tolerances).
- Cannot provide references from buyers who have verified the thickness consistency on past orders.
Conclusion
Core thickness variation is not an inevitable consequence of aluminum composite panel manufacturing. It is a preventable quality issue that arises from inadequate process control, worn equipment, or cost-cutting pressure.
For procurement professionals, the path to avoiding core thickness variation is clear: specify tight tolerances, verify supplier capabilities, inspect pre-production samples, conduct third-party in-process inspection, and include strong rejection clauses in contracts.
The cost of preventing core thickness variation—through careful supplier selection and verification—is negligible compared to the cost of receiving a shipment of inconsistent panels that cannot be installed properly. By taking proactive steps, you can ensure that every panel in your order meets the dimensional specifications required for a flat, uniform, and durable facade.