Welcome to Vbond
The Project Manager‘s Guide to Alucobond Flatness Specifications
- Alucobond flatness specification
- Panel flatness tolerance
- 2m straightedge test
- Oil canning prevention
- 15-degree viewing angle
- Alucobond ceiling panel flatness
- Thickness tolerance ±0.15mm
- Bow limit 1.5mm/m
- Site inspection checklist
- Procurement specification
- Substructure flatness
- Ceiling panel installation quality
- ACP flatness measurement
- Project manager quality control
- ALUCOBOND technical standards
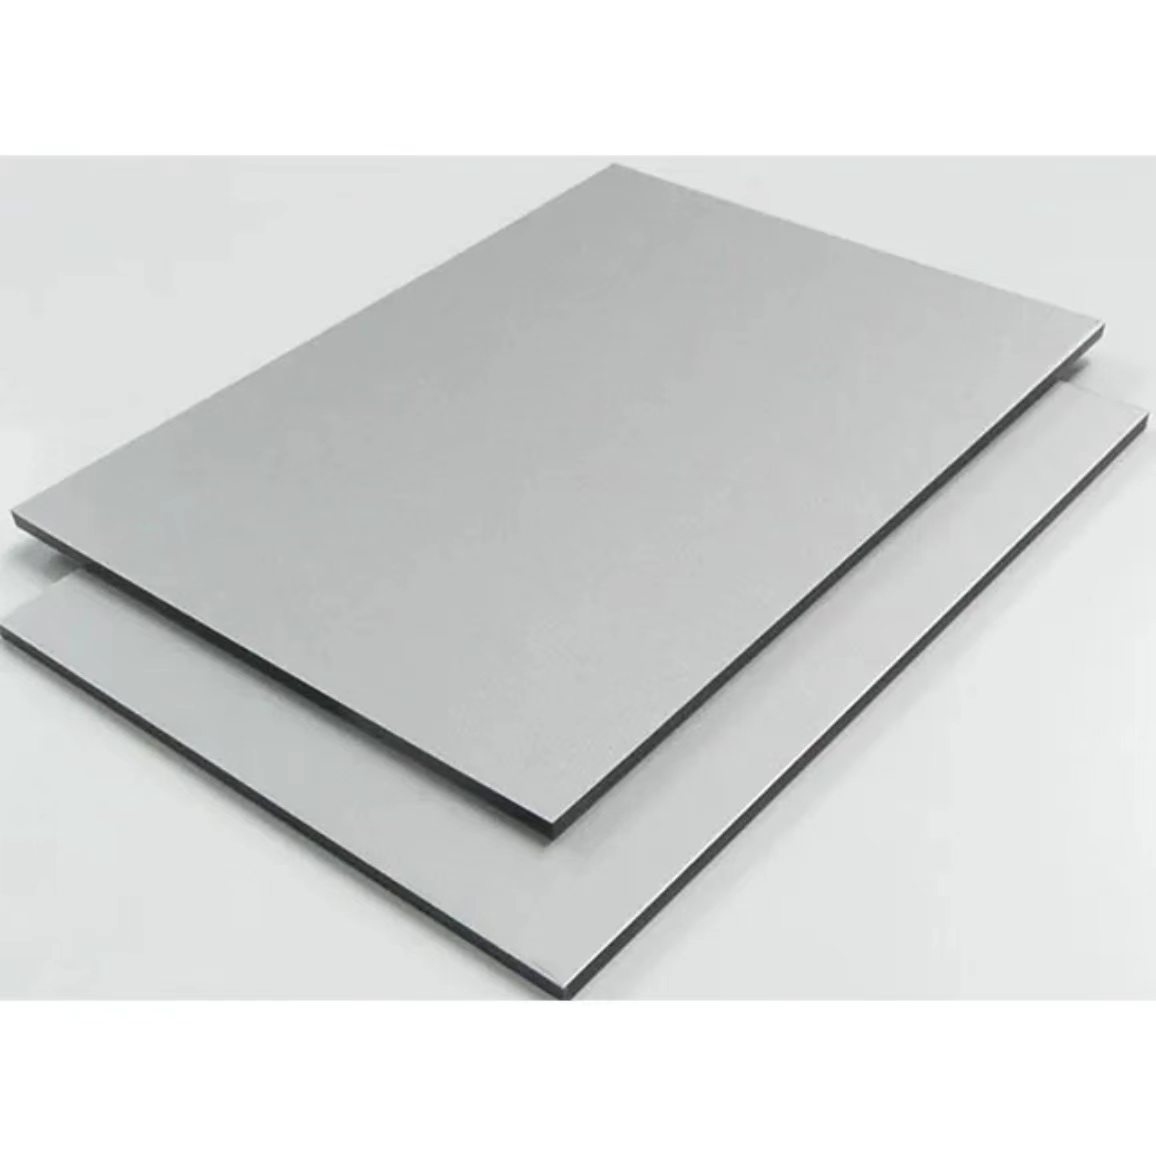
You stand on the scaffolding, squinting at the freshly installed ceiling. The light catches the surface at just the wrong angle. There it is—a subtle wave. A ripple. A distortion that nobody else sees yet. But you see it. And you know the client will see it too.
Flatness is the single most visible quality attribute of any Alucobond installation. Get it right, and the building looks like a million dollars. Get it wrong, and every imperfection screams at you every time the sun hits the facade—or the ceiling lights come on.
This guide cuts through the confusion. You will learn the actual numbers that define "flat." You will understand how to measure flatness on site. You will know what to reject and what to accept. And you will protect your project from the hidden costs of wavy panels.
Part 1: What "Flat" Actually Means — The Numbers
Flatness is not a feeling. It is a measurement. And the numbers are specific.
The ALUCOBOND thickness tolerance: ±0.15 mm
That is the official specification for total panel thickness. If the thickness varies by even 0.2 mm, the panel cannot lie flat.
Dimensional tolerances from ALUCOBOND technical data:
Parameter | Tolerance |
Panel thickness | ±0.2 mm |
Width | +6 mm |
Length (1000–4000 mm) | -0 / +6 mm |
Length (4001–8000 mm) | -0 / +10 mm |
Cover sheet displacement | Max 2 mm to one side |
Industry flatness targets for aluminum composite panels:
Standard | Tolerance |
Premium quality panels | ≤1.0–1.5 mm bow per linear meter |
General industry standard | Flatness ≤3 mm/m |
Common practice for site inspection | ≤2.0 mm over 2 m straightedge |
GB/T 17748-2016 | ≤5 mm/m for bow |
A quality Alucobond panel should not bow more than 1.0–1.5 mm per linear meter of length. Premium manufacturers hold to stricter internal standards.
Part 2: The Hidden Causes of Poor Flatness
Panels do not arrive wavy by accident. The causes are baked in during manufacturing.
The Cure Gradient Problem
ACP manufacturing involves bonding aluminum skins to a core under high heat. As the panel cools, the aluminum and core contract at different rates. If the cooling is uneven—if the top skin cools faster than the bottom—the panel will bow.
A low-quality manufacturer rushes this cooling to save money. A professional Alucobond factory controls the cooling curve tightly, ensuring dimensional stability.
Residual Stress from Rolling
Every coil of aluminum has residual stress from the rolling mill. Premium manufacturers test the aluminum chemistry (Alloy 5005) to ensure consistency. Cheap manufacturers use unknown scrap alloys. One batch may have high residual stress, while the next does not.
The "Tolerance Stack-Up" Problem
Standards like GB/T 17748-2016 allow for specific flatness tolerances. A cheap manufacturer will ship panels at the very edge of this tolerance. A premium manufacturer holds to stricter, internal standards.
What this means for you:
A panel that meets the minimum standard may still look wavy on your ceiling. If you want flat, specify tighter tolerances in your procurement documents.
Part 3: How to Measure Flatness on Site — The 2-Meter Straightedge Test
This is the standard field test for Alucobond flatness. It is simple, objective, and defensible.
Tools you need:
- 2 m straightedge (calibrated, with certification)
- Feeler gauges (set of metric gauges)
- Laser level (optional, for larger areas)
- Diffuse, non-glare lighting
- Camera for documentation
The procedure:
1. Place the straightedge on the panel surface at horizontal, vertical, and diagonal orientations
2. Measure the maximum gap between the straightedge and the panel surface using feeler gauges
3. Map readings on a 3×3 grid per panel to capture both global and local planarity
4. Span across panel joints to detect steps and lipping
5. Record results in millimeters, tie them to panel IDs and elevations
6. Photograph each measurement with the gauge size visible
The acceptance threshold:
Common practice targets ≤2.0 mm over 2 m for general flatness and tighter limits near fixings. When a reading exceeds limits, investigate the subframe first—misaligned rails, shimming gaps, or debris frequently drive nonconformance.
For a ceiling installation, the stakes are higher.
A wavy ceiling is visible from every angle. Every light fixture casts shadows that reveal imperfections. The 2-meter straightedge test is your best defense. Use it on every Alucobond ceiling panel before installation.
Part 4: The Oil Canning Problem — What the ALUCOBOND® Specification Actually Says
Oil canning is the visible waviness or rippling that can occur on the surface of flat metal panels. It does not compromise structural integrity. But it destroys visual perfection.
The official ALUCOBOND specification:
The cladding surface "shall not have any irregularities such as oil canning, waves, buckles, and other imperfections when viewed at any position but not less than at an angle of 15 degrees to the true plane of the panel".
What this means for you:
Some degree of visual imperfection is inevitable in metal cladding. But acceptable limits can be defined and enforced. The 15-degree viewing angle is your standard. If you cannot see the defect from 15 degrees off the panel plane, it passes. If you can, it fails.
For ceiling applications, this standard is even more critical.
An Alucobond ceiling panel is viewed from below. The viewing angles are different. The light is different. What looks flat from the ground may look wavy when the ceiling lights turn on. Inspect ceiling panels from the actual viewing position, not just from straight on.
Part 5: The Inspection Checklist for Project Managers
Before you sign off on any Alucobond installation—especially a ceiling installation—run through this checklist.
Pre-Installation Inspection:
Check | Method | Pass/Fail |
Panel thickness | Micrometer at multiple points | ±0.2 mm tolerance |
Panel flatness | 2 m straightedge + feeler gauges | ≤2.0 mm over 2 m |
Bow per linear meter | Straightedge along length | ≤1.0–1.5 mm/m |
Edge straightness | Straightedge along edge | ≤1 mm/m |
Surface defects | Visual inspection under raking light | No scratches, dents, or coating defects |
During Installation:
Check | Method | Pass/Fail |
Substructure flatness | Laser level + straightedge | Within project tolerance |
Panel alignment | Visual + straightedge across joints | No steps or lipping |
Fastener torque | Torque wrench | Per manufacturer specification |
Expansion gaps | Feeler gauge or ruler | Per design specification |
Post-Installation (Final Inspection):
Check | Method | Pass/Fail |
Oil canning | 15-degree viewing angle | No visible irregularities |
Ceiling panel flatness | 2 m straightedge, raking light | ≤2.0 mm over 2 m |
Joint consistency | Visual + feeler gauge | Uniform gaps |
Overall appearance | Walkthrough with client | Acceptable to all parties |
Part 6: What to Specify in Your Procurement Documents
Do not leave flatness to chance. Put the numbers in writing.
Sample specification clause:
"All Alucobond panels shall be manufactured to a flatness tolerance of ≤1.0 mm per linear meter of length. Panels shall be free from visible oil canning, waves, buckles, or other surface irregularities when viewed at any position at an angle of 15 degrees to the true plane of the panel. Thickness tolerance shall be ±0.15 mm. All panels shall be inspected on site using a 2 m straightedge and feeler gauges. Any panel exceeding the flatness tolerance shall be rejected and replaced at the supplier's expense."
Additional requirements for ceiling panels:
"Alucobond ceiling panels shall be inspected under raking light from the finished ceiling height. Any panel showing visible distortion under these conditions shall be rejected."
Part 7: Common Mistakes to Avoid
Mistake 1: Trusting the visual inspection only
Your eyes lie. What looks flat in diffuse light looks wavy in raking light.
Fix: Use the 2 m straightedge and feeler gauges on every panel. Document every measurement.
Mistake 2: Not measuring across joints
Individual panels may be flat. The joint between them may have a step. That step is visible.
Fix: Span the straightedge across panel joints to detect steps and lipping.
Mistake 3: Ignoring the substructure
A flat panel on an uneven substructure will not look flat. The panel follows the surface behind it.
Fix: Check substructure flatness before installing panels. Shim as needed.
Mistake 4: Accepting "within tolerance" without checking
"Within tolerance" and "flat enough for your project" are two different things.
Fix: Specify tighter tolerances than the minimum standard. Inspect every shipment.
Mistake 5: Forgetting the ceiling
Ceilings are different from walls. The viewing angle is different. The light is different. The stakes are higher.
Fix: Inspect Alucobond ceiling panels from the finished ceiling height. Use raking light. Be ruthless.
The Bottom Line
Flatness is not a feeling. It is a measurement. The numbers are clear: ±0.15 mm thickness tolerance. ≤1.0–1.5 mm bow per meter. ≤2.0 mm over 2 m straightedge. No visible oil canning at 15 degrees.
The tools are simple: 2 m straightedge, feeler gauges, camera. The method is straightforward: measure, document, reject if out of spec.
The stakes are high. A wavy facade costs you reputation. A wavy ceiling costs you more—because every client looks up eventually.
When you are standing under that Alucobond ceiling panel, bathed in the soft glow of architectural lighting, you will know—not hope, not guess, but know—that your ceiling is flat. Because you measured it. Because you specified the right tolerances. Because you refused to accept anything less.
That is the difference between a project manager and a great project manager. One hopes the panels are flat. The other makes sure they are.
Choose the right Alucobond ceiling panel. Specify the numbers. Measure the results. Your reputation depends on it.